The food processing industry is growing rapidly, and manufacturers are continuously looking for ways to improve production efficiency, maintain hygiene, and reduce operational costs. One of the most important components of a modern food processing plant is the conveyor system.
Conveyors help move raw materials, semi-finished products, and finished food products smoothly from one processing stage to another. From snack manufacturing to large-scale food production, conveyor systems play a vital role in ensuring smooth and continuous operations.
1. Increased Production Efficiency
Conveyor systems automate product movement between different machines, reducing unnecessary delays and improving production speed. They help maintain a continuous workflow and increase overall plant efficiency.
2. Reduced Manual Handling
Manual transportation of food products requires additional manpower and time. Automated conveyors reduce repetitive handling, minimize labour dependency, and allow employees to focus on important production activities.
3. Improved Hygiene and Food Safety
Hygiene is essential in food manufacturing. Food-grade conveyor systems, with suitable stainless steel construction and easy-to-clean designs, help maintain hygienic processing conditions and support food safety practices.
4. Reduced Product Breakage and Wastage
Delicate food products such as namkeen, chips, extruded snacks, and other fried products require careful handling. Specially designed conveyor systems ensure smooth product movement and help minimize breakage, product damage, and wastage.
5. Smooth Integration with Processing Lines
Conveyors connect different machines and operations, including frying, cooling, seasoning, weighing, and packaging. This integration creates a coordinated production line and improves overall operational performance.
6. Better Space Utilization
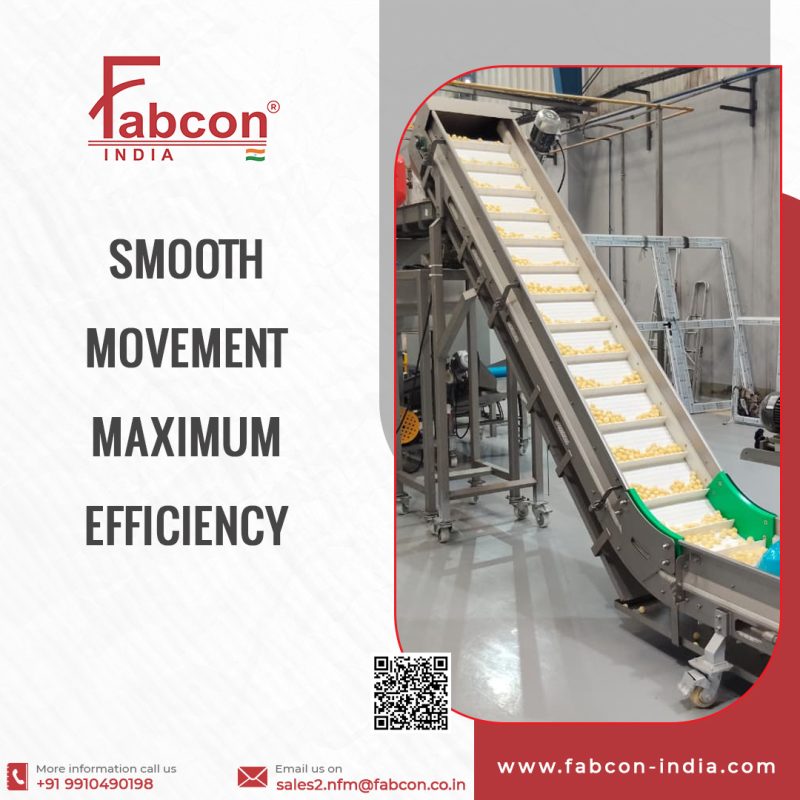
Modern conveyor systems are available in different configurations, including horizontal, inclined, and vertical designs. These solutions help manufacturers utilize factory space effectively while maintaining smooth product flow.
7. Lower Operational Costs
By reducing manual handling, product losses, and production interruptions, conveyor systems help minimize operational expenses and improve long-term manufacturing efficiency.
